Standard off-the-shelf factory automation optics are hitting a hard technical ceiling. Modern assembly lines now deploy image sensors exceeding 100 megapixels, with pixel pitches shrinking below 2.0 microns. When automated inspection lines run at dozens of frames per second, stock optical components frequently introduce chromatic aberration, field curvature, and image degradation that confuse downstream deep-learning models.
High-precision automated sorting, semiconductor packaging, and biomedical inspection now demand specialized optical solutions. Engineering teams can no longer settle for generic components when dimensional tolerances are measured in fractions of a millimeter. Sourcing custom FA lenses has transitioned from a niche requirement to a standard development track for machine vision integrators.
Optical manufacturers such as Jinyuan work directly with machine builders to design, prototype, and mass-produce vision assemblies tailored to tight mechanical envelopes. If your engineering group is preparing a vision architecture for an upcoming production cycle, you can submit your technical specifications directly to our engineering team for a targeted optical assessment and quotation.
Use the following checklist to define parameters, assess manufacturing capabilities, and manage the sourcing pipeline for your custom optical systems.
Phase 1: Defining Optical and Mechanical Parameters
A failed optical sourcing project almost always traces back to an incomplete initial specification. Before contacting optical design houses, you must define the boundary conditions of your vision system with precision.
Sensor Compatibility and Format Matching
Your sensor defines the boundary of your optical requirements. Match your lens parameters to the sensor layout using these critical metrics:
- Image Circle Diameter: Ensure the lens covers the full active sensor format (e.g., 1/1.8", 2/3", 1.1", APS-C, or 35mm full-frame) without vignetting.
- Pixel Pitch and Cutoff Frequency: When pixel pitch drops below 2.5 µm, your lens requires higher resolving power. Calculate the Nyquist limit using the formula fNyquist = 1 / (2 × Pixel Pitch) to establish your baseline spatial frequency requirements.
- Chief Ray Angle (CRA) Matching: Ensure the lens CRA closely matches the sensor micro-lens acceptance angle. A severe mismatch creates severe corner shading and color crosstalk.
Core Optical Performance Metrics
Do not simply specify "high resolution." Quantify optical performance using verifiable physical measurements across the entire field of view:
- Modulation Transfer Function (MTF): Specify MTF contrast values at specific spatial frequencies (e.g., >30% contrast at 140 lp/mm across 90% of the field). You can review technical definitions of spatial frequency and contrast via the Modulation Transfer Function standards.
- Optical Distortion: Differentiate between TV distortion and geometric radial distortion. For metrology, require radial distortion below 0.05% or switch to a bilateral telecentric optical layout.
- Working Distance (WD) and Conjugate Distance: Fix your minimum and maximum working distance early. Optical designs optimized for infinite conjugate distances will suffer severe spherical aberration when focused at short working distances without floating elements.
- Relative Illumination: Demand corner illumination exceeding 70% to prevent artificial contrast drops that trigger false rejects in machine learning algorithms.
Spectral Bandwidth and Specialized Coatings
Modern automated inspection frequently extends outside the visible spectrum. Specify antireflection (AR) coatings according to your illumination wavelengths:
- Visible (VIS): 400 nm to 700 nm for standard color and monochrome sorting.
- Visible to Near-Infrared (VIS-NIR): 400 nm to 1000 nm with chromatic correction (achromatic or apochromatic designs) to prevent focal shift when switching illumination.
- Short-Wave Infrared (SWIR): 900 nm to 1700 nm for silicon wafer inspection, agricultural moisture detection, and solar cell manufacturing.
Mechanical Envelope and Ruggedization
A factory floor will quickly degrade lab-grade optical hardware. Ruggedized FA lenses eliminate moving parts that shift under industrial mechanical stress:
- Aperture and Focus Locking: Replace standard manual thumb screws with recessed set screws or fixed-aperture spacer rings.
- Anti-Vibration and Shock Resistance: Demand glued internal element groups to maintain optical centering under continuous mechanical acceleration.
- Thermal Compensation (Athermalization): Use matched mechanical housings (e.g., invar or tailored aluminum-plastic sleeves) to stabilize focal performance across industrial temperature ranges (-20°C to +60°C).
Phase 2: Choosing Between the OEM and ODM Sourcing Route
Deciding between modifying an existing optical assembly (OEM) or developing an entirely new design from scratch (ODM) dictates your non-recurring engineering (NRE) budget, timeline, and intellectual property standing.
The OEM Route: Modification of Proven Platforms
The OEM path takes an established base lens and modifies select mechanical or optical subassemblies. This approach delivers distinct advantages for projects with aggressive deadlines:
- Typical Timeline: 4 to 8 weeks for physical prototypes.
- NRE Costs: Minimal to moderate, primarily covering new barrel machining, mount adapters (such as M12, C-mount, CS-mount, or F-mount), or custom optical filter integration.
- Best Suited For: Projects where an existing focal length and optical prescription are acceptable, but you require vibration dampening, custom water-resistant enclosures, or proprietary optical coatings.
The ODM Route: Full Custom Optical Design
The ODM path begins with a blank optical schematic in software. This approach solves complex optical challenges when off-the-shelf mechanics cannot meet physical space limitations or severe optical specifications:
- Typical Timeline: 16 to 26 weeks from optical simulation to pilot production.
- NRE Costs: Substantial, covering optical ray tracing, tolerance budgeting, dedicated tooling, test fixtures, and optical melt-run sourcing.
- Best Suited For: Deeply integrated embedded vision systems, multi-sensor optical pods, non-standard spectral bands, or extreme form factors.
Intellectual Property (IP) and Exclusivity
Ensure your development contract explicitly specifies ownership of critical technical assets. Clarify whether your firm retains the rights to:
- The optical prescription (lens radii, element thicknesses, and glass catalog selections).
- The mechanical housing CAD files and assembly drawings.
- Custom test fixtures and optical metrology alignment tools.
Phase 3: Auditing the FA Lens Manufacturer
Not every precision optics shop can reliably produce industrial-grade FA lenses. A comprehensive supplier audit must examine both software design capabilities and manufacturing equipment.
During the design phase, optical suppliers must demonstrate strong simulation competency. Ask candidates for sample tolerance analyses generated in optical design packages like Ansys Zemax OpticStudio or Synopsys CODE V. The supplier must show Monte Carlo yield simulations that reflect realistic shop-floor manufacturing variations, rather than idealized theoretical models.
Evaluate the manufacturer's physical production assets. Precision lens fabrication requires advanced processing machinery, including CNC spherical and aspherical polishing systems, deterministic micro-grinding equipment, and automated ultrasonic cleaning lines.
Metrology capabilities are equally critical. Your partner must verify production quality against international standards such as ISO 10110 for optical elements and systems. Confirm the presence of dedicated metrology instruments on the factory floor:
- Modulation Transfer Function Testers: Automated MTF test equipment (such as Trioptics ImageMaster) for on-axis and off-axis performance measurement.
- Laser Interferometers: Phase-shifting interferometers (such as Zygo Verifire) to measure transmitted wavefront error and surface accuracy.
- Optical Centering Stations: Instruments to control lens tilt and decentration down to single-digit arcseconds during assembly.
Jinyuan maintains stringent cleanroom environments alongside automated optical test stations to guarantee that every lens cell meets tight optical tolerances. Our integrated production lines handle every stage from raw glass blank processing to final MTF qualification.
Phase 4: Prototyping, Validation, and Quality Assurance
Bridging the gap between engineering samples and volume production requires a structured verification process. Avoid authorizing full production runs based on hand-tuned lab prototypes.
Golden Sample Sign-Off
The first physical batch must yield a designated "Golden Sample" set. These units represent the benchmark for all future production lots:
- Review complete coordinate measuring machine (CMM) reports for all critical mechanical mounting surfaces and thread tolerances.
- Review individual transmitted wavefront error (WFE) profiles and full-field MTF scan data.
- Seal and archive a master reference unit at both the customer facility and the manufacturer facility.
Industrial Reliability Testing
Subject validation samples to destructive and non-destructive environmental stress tests according to industrial testing protocols, such as IEC 60068 environmental testing standards:
- Vibration and Shock Resistance: Subject the lens to multi-axis sinusoidal and random vibration profiles to simulate operation on high-speed robotic end-effectors.
- Thermal Shock and Cycling: Cycle assemblies rapidly between storage and operational temperature extremes to detect thermal expansion mismatches between glass elements and metallic housings.
- Ingress Protection: Verify IP65 or IP67 sealing using positive pressure decay testing if the optics operate in wash-down or particulate-heavy factory environments.
Batch-to-Batch Consistency
Maintain control over production consistency by negotiating statistical process control (SPC) milestones. Demand documented Cp and Cpk values for critical quality parameters like back focal length (BFL), optical axis runout, and resolving power across volume deliveries.
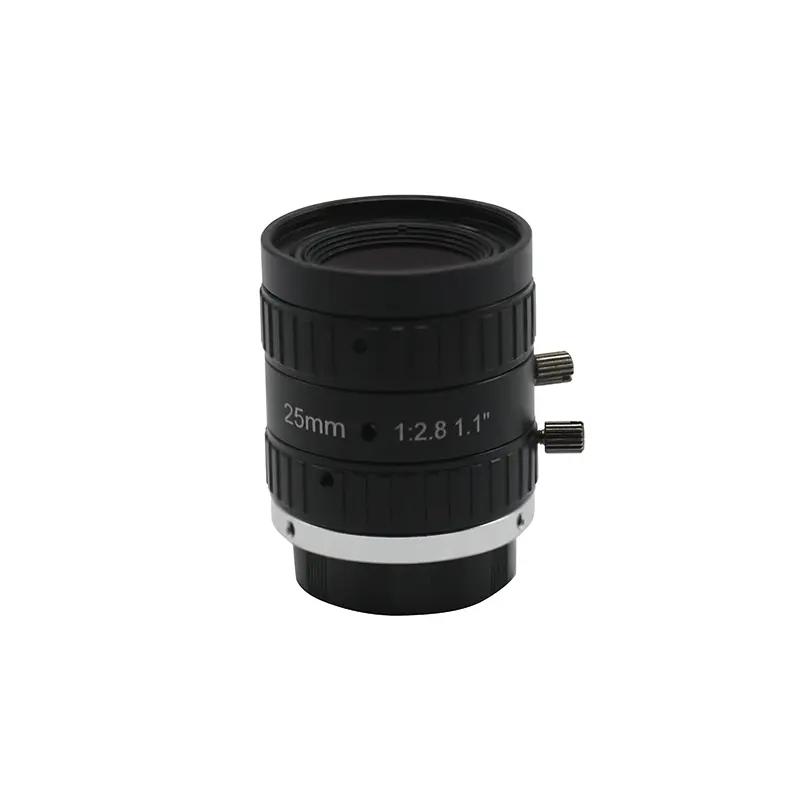
Technical Trends Influencing FA Lenses in 2026
Several optical engineering shifts are reshaping custom industrial vision programs this year:
- Liquid Lens Integration: Electronically focus-tunable lenses are moving directly into custom industrial optical designs. Integrating electrowetting elements allows sub-millisecond focus adjustments across wide object distance variations without mechanical drive motors.
- Built-In Polarization Filtration: Polarized sensors require matching low-stress, birefringence-free optical assemblies. Custom FA lenses now integrate multi-layer anti-reflective coatings and zero-stress glass elements to preserve polarization vectors for glare-free surface defect inspection.
- Miniaturized Micro-Optics for Embedded Compute: Edge AI vision platforms demand ultra-short total track lengths (TTL). Designers are leveraging molded glass aspheric surfaces to collapse complex 10-element spherical stacks down to compact 5-element assemblies without sacrificing resolving power.
Sourcing Checklist Summary
Keep these fundamental checkpoints accessible when drafting your optical development plan:
- Sensor format, pixel pitch, and target MTF frequency fully documented.
- Mechanical housing constrained with ruggedized locking mechanisms.
- Thermal operating range modeled via optomechanical tolerance budgets.
- Supplier cleanroom standards, metrology assets, and ISO compliance verified.
- IP rights, tooling amortizations, and production scaling terms finalized.
Procuring custom FA lenses demands close technical collaboration between optical designers and mechanical automation engineers. Treating your supplier as an integrated technical partner ensures your machine vision platforms deliver reliable, repeatable inspection data year after year.
Jinyuan delivers custom optical assemblies designed to survive demanding industrial automation environments. Speak with an optical specialist today to review your project specifications, request technical engineering support, or submit your bill of materials for a competitive manufacturing quote.
Frequently Asked Questions
Q1: What are the typical non-recurring engineering (NRE) costs for custom FA lenses?
A1: OEM modifications (such as changing barrel interfaces, adjusting aperture stops, or adding specialized optical filters) typically incur NRE charges between $2,000 and $8,000. Full ODM optical programs (including ray-tracing design, mechanical barrel engineering, custom glass tooling, and test fixtures) generally range from $15,000 to over $60,000, depending on the complexity of aspheric surfaces, spectral requirements, and production volume commitments.
Q2: How does pixel pitch dictate lens MTF requirements?
A2: The sensor pixel pitch determines the Nyquist cutoff frequency (calculated as 1 / (2 × Pixel Pitch)). For example, a modern sensor with a 2.4 µm pixel pitch has a Nyquist limit of roughly 208 line pairs per millimeter (lp/mm). The lens must maintain adequate contrast (typically 20% to 30% MTF or higher) at that spatial frequency to fully utilize the sensor's native resolving capabilities without introducing optical blur.
Q3: Can standard C-mount FA lenses handle high-vibration robotic arms?
A3: Standard commercial off-the-shelf C-mount lenses frequently fail on robotic arms. Their internal spring-loaded iris mechanisms, movable focus groups, and simple thumb screws will loosen, causing focus drift, pixel shift, and optical decentration. Robotic installations require ruggedized FA lenses that feature glued element groups, clamping lock rings, or fixed mechanical spacer configurations.
Q4: What is the difference between optical distortion and TV distortion in machine vision?
A4: Optical distortion (geometric radial distortion) measures the displacement of image points from their theoretically ideal positions across the field, modeled via mathematical polynomial equations. TV distortion is a simplified industrial workshop metric that measures the curvature of a straight line along the edge of the image frame as a percentage of image height. Precise automated metrology requires true geometric distortion values below 0.1% across the full image diagonal.
Q5: Why is SWIR compatibility becoming critical for custom factory automation optics?
A5: Short-wave infrared (SWIR) imaging allows machine vision systems to see through opaque packaging, detect sub-surface cracks in silicon wafers, identify liquid fill levels through plastic containers, and spot moisture variations in agricultural products. Designing custom FA lenses for SWIR requires specialized optical glass with high transmission beyond 1000 nm and proprietary broadband anti-reflective thin-film coatings.